Solutions · Sustainability & ESG
Condensate Water Recovery: high-purity thermal water back to boiler makeup
Polishing condensate for lower makeup, energy, and chemical oxygen scavenger demand—simple heat balance wins.
Use when
Blowing condensate to drain wastes heat and drives extra makeup treatment.
Process options
Polishing, oxygen control, and leak detection on return headers.
Assessment output
Fuel and chemical savings with documented mass and energy balance.
Inputs and conditions for an assessment
Collect feed variability, capacity, target quality, operating hours, discharge or reuse boundaries and installed equipment data. Compare examples on matched conditions and meter boundaries; assess a project using actual water data, equipment documentation and any necessary tests.
View the process illustration
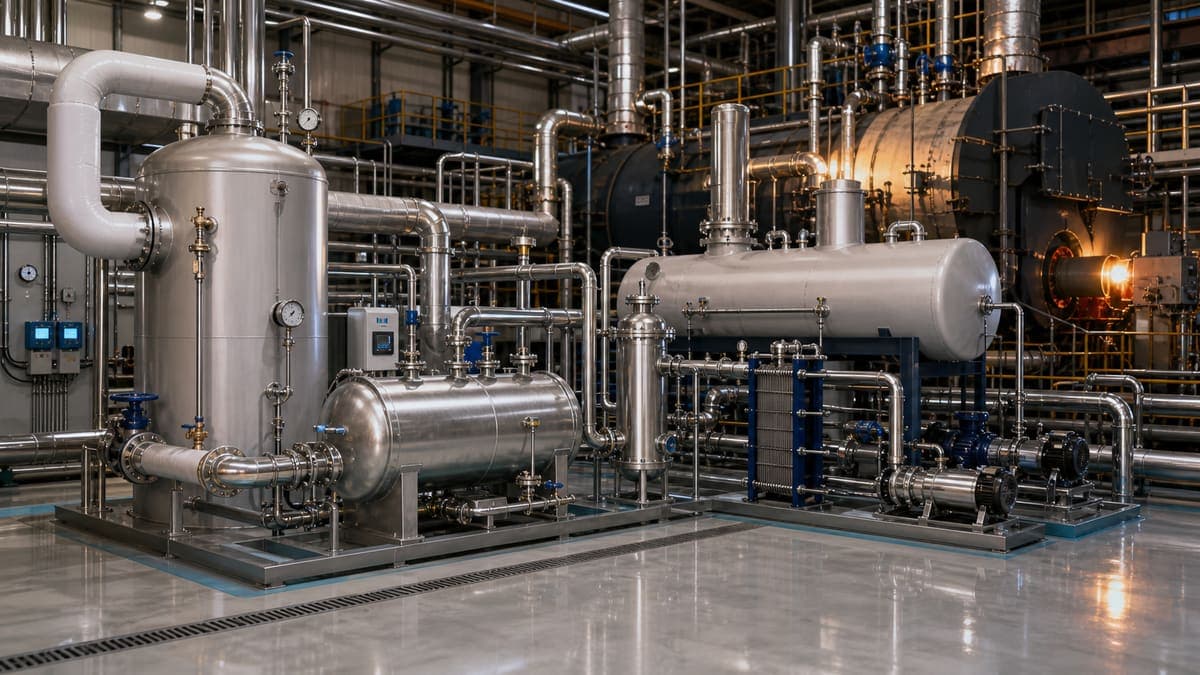
Condensate Water Recovery: high-purity thermal water back to boiler makeup
In the industrial landscape of 2026, efficient resource management is no longer merely an operational advantage—it's a critical component of corporate resilience, particularly for industries navigating stringent export-market ESG requirements in the UK and EU. At the nexus of energy and water stewardship lies condensate recovery: the strategic capture and reuse of high-purity, high-temperature water from steam systems. This isn't just about saving a drop; it's about reclaiming a vital, thermally charged resource that directly impacts your carbon footprint, reduces water withdrawal from increasingly stressed sources, and fortifies your operational independence against escalating water risks.
The steam generated in boilers and used for process heating, power generation, or humidification invariably condenses back into water. This condensate, often overlooked or discharged, represents a significant hidden asset. Its inherent purity, having been distilled, means less treatment is required compared to fresh makeup water. Crucially, its elevated temperature translates directly into substantial energy savings when returned to the boiler, bypassing the need to heat colder fresh water from scratch. For companies facing the scrutiny of supply chain sustainability assessments and CO2 reporting, optimising condensate return is a tangible, data-driven pathway to demonstrating responsible resource management and achieving ambitious decarbonisation goals.
Worked energy / carbon sketch
Illustrative Assumptions:
- Condensate flow rate: 50 cubic meters per hour (m³/h)
- Annual operating hours: 8,000 hours per year
- Average condensate return temperature: 80°C
- Average fresh makeup water temperature: 15°C
- Specific heat capacity of water: 4.18 kJ/kg·°C (approx. 1.16 Wh/kg·°C)
- Energy required for fresh water treatment (RO/demineralisation): 5 kWh/m³ (illustrative for high-purity water)
- Grid electricity carbon intensity (illustrative assumption): 0.233 kg CO₂e/kWh; use the reporting-year factor applicable to the actual electricity supply.
Calculation of Annual Energy Savings:
-
Heat Energy Saved:
- Temperature difference: 80°C - 15°C = 65°C
- Energy saved per m³ (1000 kg): 1000 kg * 1.16 Wh/kg·°C * 65°C = 75,400 Wh/m³ = 75.4 kWh/m³
- Annual heat energy savings: 50 m³/h * 8,000 h/year * 75.4 kWh/m³ = 30,160,000 kWh/year
-
Water Treatment Energy Saved:
- Annual water treatment energy savings: 50 m³/h * 8,000 h/year * 5 kWh/m³ = 2,000,000 kWh/year
-
Keep the Energy Streams Separate:
- The estimated 30,160,000 kWh/year of recovered heat and 2,000,000 kWh/year of avoided treatment electricity replace different energy inputs. Account for return-line heat losses, condensate polishing and return-pump electricity before reporting net savings.
Calculation of Annual Carbon Emissions Avoided:
- Avoided treatment-electricity emissions: 2,000,000 kWh/year * 0.233 kg CO₂e/kWh = 466,000 kg CO₂e/year, or 466 tonnes CO₂e/year, before additional return-system electricity.
- Avoided boiler-fuel emissions = net recovered heat / marginal boiler efficiency * the applicable fuel emission factor. Keep the efficiency and fuel factor on the same heating-value basis; they have not been specified here, so a total emissions reduction cannot yet be calculated.
This illustrative balance separates thermal recovery from electricity savings. Measure condensate flow, return temperature, losses and incremental pumping or polishing loads, then apply site-specific fuel and electricity factors. The US Department of Energy condensate-return tip sheet explains how returned heat reduces boiler fuel demand. Water, chemical and discharge savings can be evaluated separately from the energy balance.
Traditional vs engineering evaluation path
| Topic | Dump / light strainer return | Polished high-purity return (engineering evaluation path) |
|---|---|---|
| Heat | Flash losses; cold makeup reheated from scratch. | Hot, stable return; fuel and blowdown both drop. |
| Water | Extra demin water make-up and effluent. | Maximises closed steam loop; lower intake m³. |
| Proof | Sparse iron/silica trending. | Instrumented conductivity, sodium, silica for ESG files. |
Carbon savings calculator (illustrative)
Estimate annual changes in electricity use and CO₂e emissions from specific energy before and after a change. Replace defaults with site meter data and the grid emission factor required by your utility or ESG methodology.
Annual electricity reduction = flow × annual operating hours × (specific energy before − after). Emissions reduction = electricity reduction × grid factor / 1000. Negative values indicate an increase.
ΔkWh = Q × H × (SEC₀ − SEC₁) · ΔtCO₂e = ΔkWh × EF / 1000
Specific energy reduction: 1.00 kWh/m³
Estimated electricity savings: 800,000 kWh / year
Indicative avoided emissions: 336 tCO₂e / year
Related equipment & product lines
These categories typically support the approach above—open any line to compare brands and models.
- Heat ExchangersThermal exchange equipment for process integration and temperature management.View category →
- Ion Exchange ResinsCation/anion and mixed bed resin solutions for demineralization and polishing.View category →
- ChemicalsAntiscalants, cleaners, and process chemicals for water treatment operations.View category →
For a closer review, use the engineering inquiry form to share feed, capacity, target, and project stage. Submission does not constitute a completed design or performance commitment.